
Managing Remote Apparel Quality Control: 2026 Guide

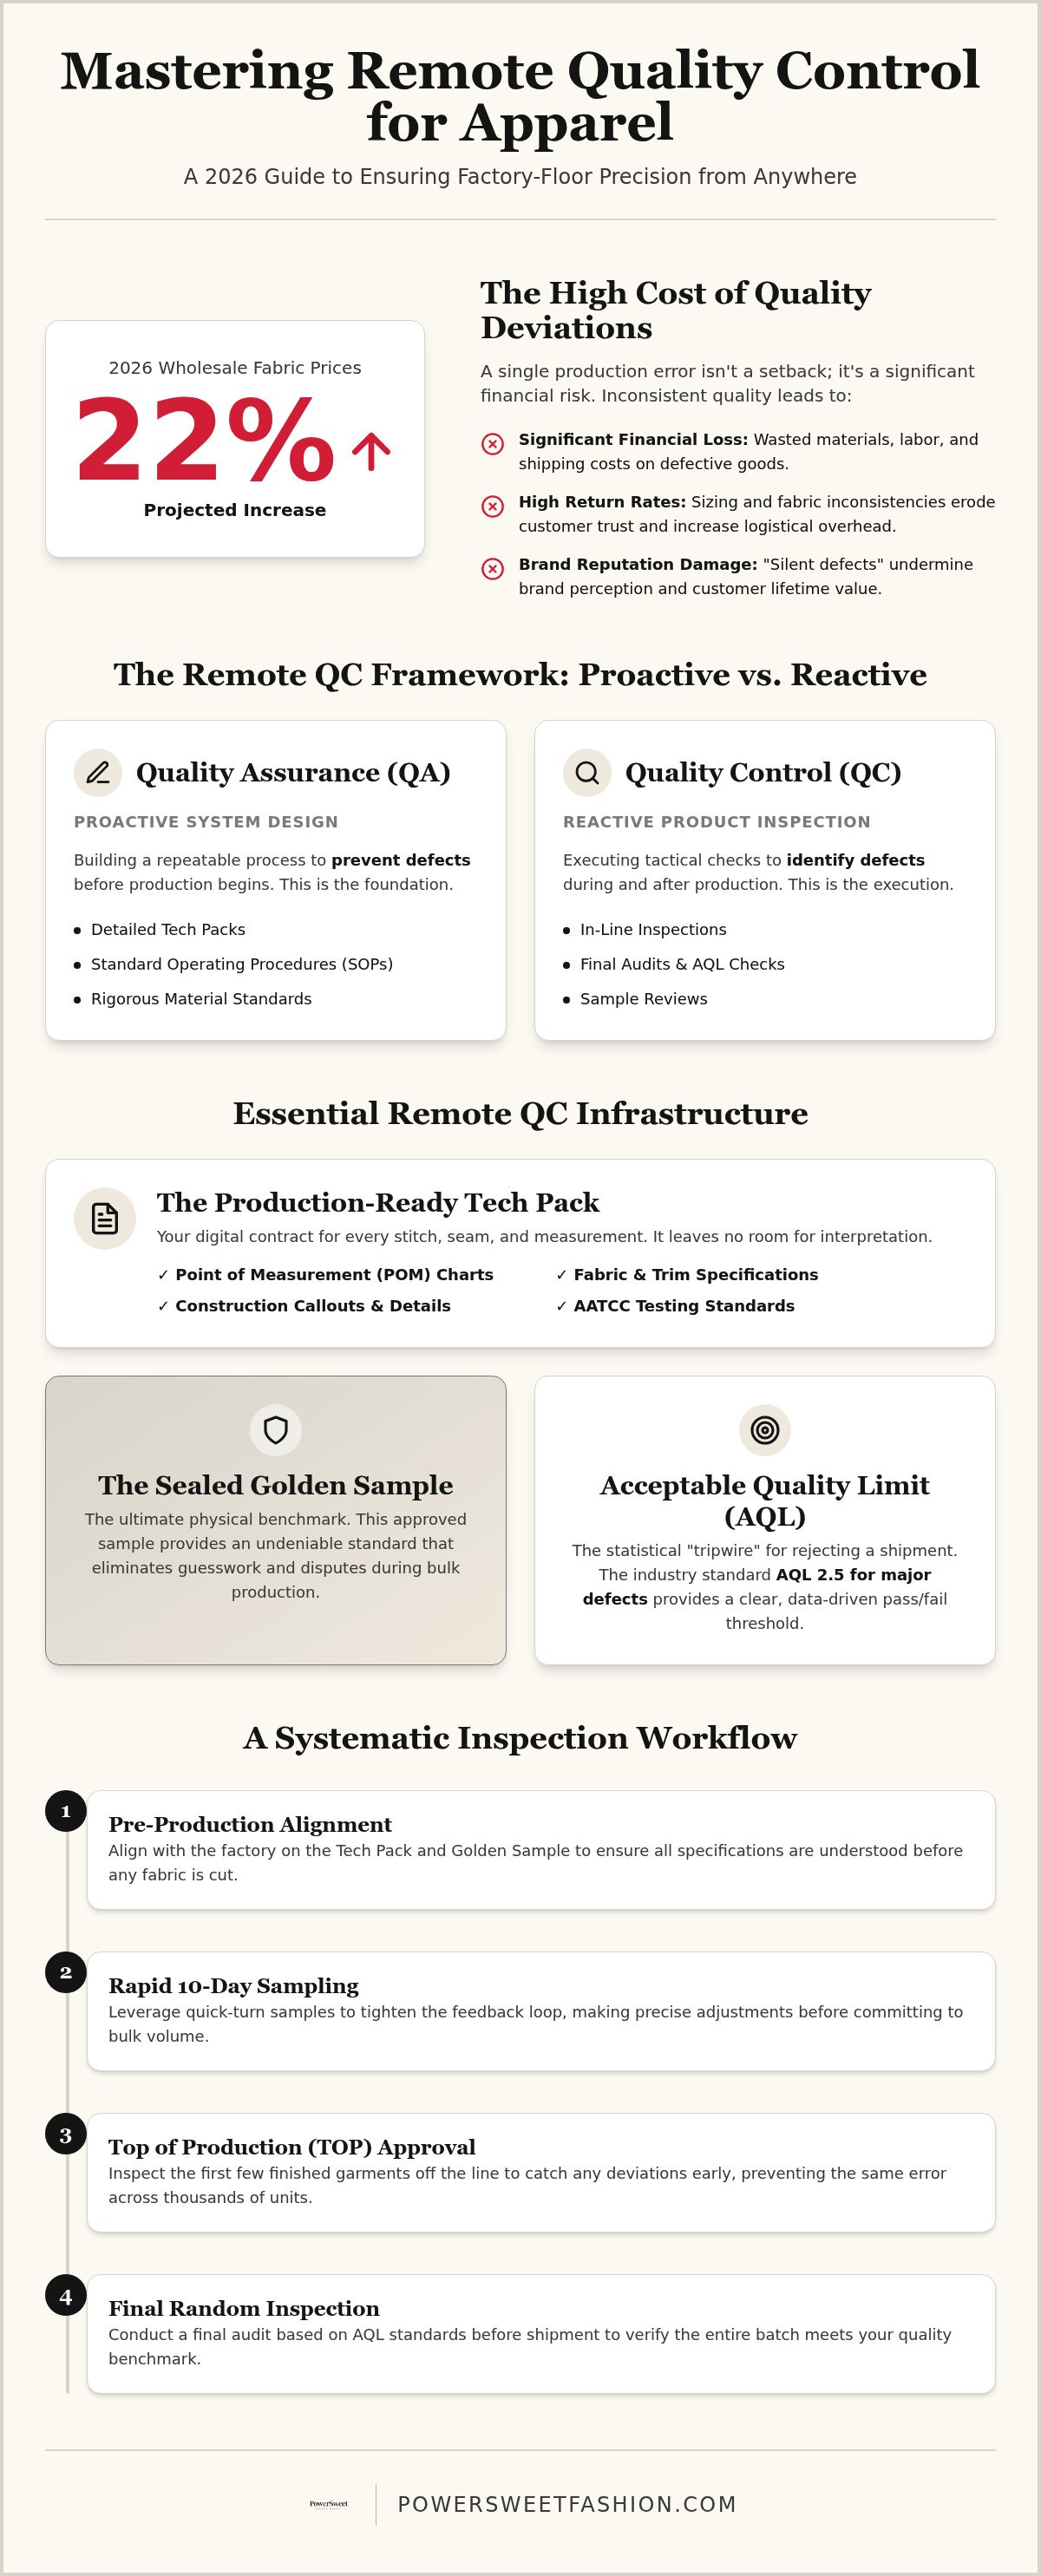
With wholesale fabric prices rising as much as 22% in 2026, a single production error isn't just a minor setback; it's a significant financial risk to your brand's growth. You likely know the anxiety of waiting for a bulk shipment, wondering if the sizing will be consistent or if the fabric hand-feel matches your approved sample. Managing remote quality control for apparel often feels like a gamble when you aren't physically standing on the factory floor to catch deviations before they become costly defects.
It's frustrating to deal with high return rates caused by miscommunications that could have been prevented with better oversight. We've developed this guide to help you master the frameworks, digital tools, and communication strategies required to ensure factory-floor precision from anywhere in the world. You'll learn how to implement a repeatable system for remote oversight that lowers defect rates and builds a trusted, transparent partnership with your manufacturer. We'll walk through the essential 2026 compliance updates, including the mandatory CPSC eFiling system, and show you how to turn your tech pack into a foolproof quality roadmap.
Table of Contents
Why Remote Quality Control is the Backbone of Modern Apparel Scaling
The Remote QC Infrastructure: Essential Documentation and Standards
Comparing Remote QC Models: Third-Party vs. Factory-Direct Oversight
The Step-by-Step Guide to Managing Remote Apparel Inspections
Leveraging PowerSweet Fashion’s Transparency for Remote Success
Why Remote Quality Control is the Backbone of Modern Apparel Scaling
Your reputation is only as strong as your last shipment. In the digital-first fashion market, "silent" defects like inconsistent seam tension or a slightly off-grain fabric don't just lead to one-time returns. They erode customer lifetime value and trigger expensive restocking logistics that can stall a growing brand. Managing remote quality control for apparel is the operational foundation that allows you to scale without losing the precision that defines your brand. By bridging the gap between your creative vision and the industrial reality of the factory floor, you ensure that what the customer sees on screen is exactly what they receive in the mail.
The Financial Impact of Quality Deviations
With wholesale fabric prices increasing by up to 22% in 2026, material waste is a critical financial threat. A failed production run isn't just lost time; it's a massive hit to your bottom line. High return rates often stem from sizing inconsistencies that could have been avoided through professional pattern making during the development phase. Your Minimum Order Quantity (MOQ) also significantly influences your risk profile. While large orders offer economies of scale, they amplify the cost of a quality failure. Utilizing flexible, low MOQs allows for tighter oversight and iterative improvements, making it a strategic choice for brands that prioritize meticulous care over raw volume.
Defining Quality Assurance (QA) vs. Quality Control (QC)
To succeed remotely, you must distinguish between building a safe system and checking the final product. Quality Assurance (QA) is the proactive design of your production workflow. This includes detailed Tech Packs, Standard Operating Procedures (SOPs), and rigorous material standards established before a single stitch is sewn. In contrast, quality control (QC) is the tactical execution of those standards through in-line inspections and final audits. Successful remote brands don't just react to problems; they design them out of the process. By treating your manufacturer as a transparent partner, you can oversee both QA and QC through digital documentation and real-time communication. This ensures that managing remote quality control for apparel remains a systematic, data-driven process rather than a game of chance. This transition from a reactive "inspection" mindset to proactive "assurance" is what builds a "safe pair of hands" partnership, allowing you to focus on growth while the factory maintains the technical precision of your original vision.
The Remote QC Infrastructure: Essential Documentation and Standards
Precision matters. Without a clear technical roadmap, you're essentially asking the factory to guess your expectations. Managing remote quality control for apparel requires a digital and physical infrastructure that leaves no room for interpretation. This foundation begins with your Tech Pack. It's more than a design file; it's your remote contract for every stitch, seam, and button placement. When you can't be on-site, these documents act as your eyes and ears on the production line.
The Anatomy of a Production-Ready Tech Pack
A professional tech pack must include exhaustive Point of Measurement (POM) charts and construction callouts. These details prevent the "close enough" mentality that often leads to sizing inconsistencies across different batches. Your fabric and trim specifications should reference AATCC testing standards to ensure colorfastness, shrinkage control, and durability. Professional sample development is critical during this phase because it identifies tech pack errors before you commit to bulk production. It's much cheaper to fix a measurement error on a single sample than on a thousand finished garments.
Before production starts, establish your Acceptable Quality Limit (AQL) standards. In 2026, the industry standard remains the statistical sampling model. Most growing brands use AQL 2.5 for major defects, which serves as a clear "tripwire" for rejecting a shipment. Defining these levels early ensures that both you and the factory have a shared understanding of what constitutes a pass or a fail.
The Power of the Sealed Golden Sample
The "Sealed Golden Sample" serves as the ultimate legal and technical benchmark, representing the exact physical standard the factory must replicate. You must have two identical approved samples: one stays with you, and the other is "sealed" and kept at the factory. This allows for real-time remote video comparisons during in-line inspections. You can hold your sample up to the camera while the inspector does the same with a piece from the line. Signing and dating these samples is vital to prevent "standard drift," where quality slowly declines over multiple production cycles.
Modern digital tools like Techpacker or integrated PLM systems allow for real-time visual reporting. These platforms bridge the distance by providing a central hub for photos, defect logs, and production updates. If you're looking for a partner who prioritizes this level of technical transparency, consider how our quality-first manufacturing approach can protect your brand's integrity. By combining physical benchmarks with digital tracking, managing remote quality control for apparel becomes a manageable, data-driven process.
Comparing Remote QC Models: Third-Party vs. Factory-Direct Oversight
Choosing the right oversight model is a strategic pivot point for any brand managing remote quality control for apparel. While the goal is always a defect-free shipment, the method of achieving it depends on your production volume, the complexity of your designs, and the depth of your relationship with the manufacturer. You generally have two primary paths: hiring an external auditor or collaborating directly with the factory's internal team. Each has a specific role in a modern supply chain, and the best choice often depends on your current stage of growth.
Independent third-party inspectors offer a layer of unbiased verification, which is particularly useful when you're working with a new factory for the first time. However, these services come with high per-visit fees and often lack the design context of your specific brand. On the other hand, the "Factory-Direct" model leverages the manufacturer's own QC team. This model is often more efficient because the inspectors are already familiar with your technical requirements and construction nuances. For many growing brands, low MOQ manufacturers provide a middle ground by offering more personalized, meticulous oversight that larger facilities might overlook.
When to Hire an Independent Auditor
Third-party intervention is most effective during specific "trigger points," such as your first production run with a new partner or when launching a product with highly complex construction. An external auditor provides a fresh set of eyes to verify that the factory's internal standards align with your AQL targets. They can also facilitate specialized lab testing for fabric composition and colorfastness, ensuring the materials meet your specific durability requirements. While valuable, remember that an auditor is a temporary observer; they don't have the same long-term interest in your brand's success as a dedicated production partner. For high-volume orders, a hybrid approach—using third-party audits for final random inspections while relying on the factory for in-line checks—can provide the best balance of cost and security.
Building Trust in Factory-Led Quality Control
Transitioning to factory-led QC requires a thorough vetting of the manufacturer's internal processes during the onboarding phase. Ask for their standard operating procedures and evidence of their internal defect logs. A partner who embraces "Open-Door Transparency" will often offer live video walkthroughs of the production line, allowing you to see the work in progress in real-time. This level of access is a hallmark of a reliable end-to-end production partner. Because they manage everything from fabric sourcing to final packing, they have more "skin in the game" to ensure every garment meets the approved standard. This collaborative approach turns the factory from a mere vendor into a safe pair of hands for your creative vision, making managing remote quality control for apparel a joint venture rather than a constant battle.
The Step-by-Step Guide to Managing Remote Apparel Inspections
Managing remote quality control for apparel requires a disciplined, chronological workflow. It's not just a final audit; it's a series of strategic gates that prevent minor deviations from becoming bulk disasters. By following a structured process, you maintain technical oversight without needing to be physically present on the factory floor. This systematic approach ensures that every production milestone serves as a checkpoint for precision and reliability.
The Pre-Production Meeting (PPM)
Alignment is the goal. Before the first cut is made, schedule a video call with the production manager to review the Sealed Golden Sample. You must confirm the "Critical to Quality" (CTQ) points, such as specific seam strengths or delicate embroidery details that are prone to error. Establish a clear communication cadence now. Daily updates via WhatsApp or Slack ensure that small questions don't turn into large mistakes, keeping the project on its 15-20 day bulk production timeline.
Remote Fabric and Trim Approvals
Consistency starts with materials. Request "Top of Production" (TOP) samples to verify that the bulk fabric sourcing matches your approved strike-offs exactly. Use high-resolution macro photography to inspect weave density and texture. For functional components, mandate a "pull test" protocol for buttons, zippers, and labels to ensure they meet safety and durability standards. This prevents the "close enough" substitutions that can lead to high return rates later.
In-line and Final Inspections
Catch errors while they're still fixable. Conduct an in-line inspection when production is 20-30% complete to verify construction and sizing. This allows for course correction while the majority of the order is still on the machines. Finally, perform a Final Random Inspection (FRI) based on your AQL standards before the shipment leaves the facility. This is your last chance to catch defects before they reach your warehouse. By mastering these steps, managing remote quality control for apparel becomes a repeatable system rather than a stressful gamble.
Visual Inspection via Video and High-Res Imagery
Documentation is your defense. Require the factory to use a standardized lighting environment for all photo reviews to ensure color accuracy. Have them place measurement tapes directly in the photos to verify Points of Measurement (POMs) against your tech pack. During a live video walkthrough, look beyond the individual garment; observe the organization of the sewing floor and the handling of finished goods. This transparency bridges the gap between digital communication and physical reality, ensuring your vision is executed with meticulous care.
If you want a partner who masters this level of detail and transparency, start your production journey with us to ensure every stitch meets your brand's standards.
Leveraging PowerSweet Fashion’s Transparency for Remote Success
Managing remote quality control for apparel requires a partner that doesn't hide behind a digital curtain. We provide an open-door philosophy that bridges the gap between your office and our factory floor. By offering direct communication and real-time oversight, we ensure your creative vision is never lost in translation. Our system prioritizes empirical reliability, giving you the data you need to make informed decisions about your brand's future. This transparency lowers the barrier to entry for growing labels, turning the manufacturing world from a mystery into a manageable, systematic process.
Speed is a critical component of quality. Our 10-day sampling process accelerates the feedback loop, allowing you to identify and correct potential issues before they reach the bulk stage. This rapid turnaround ensures that your "Sealed Golden Sample" is perfected quickly, setting a high standard for the 15-20 day production cycle that follows. We manage bulk women’s clothing production with meticulous internal standards that treat every garment as a reflection of our joint success. We don't just check for defects at the end; we build quality into every minute of the production journey through a "numbers-first" approach to reliability.
Expert Pattern Making and Sample Precision
Our in-house pattern makers are the first line of defense against quality deviations. By creating precise foundations from the start, we ensure consistency across all custom women’s clothing categories. This technical expertise allows us to reduce lead times without compromising the final audit. We don't just follow a tech pack; we optimize it for industrial efficiency and aesthetic precision. This proactive approach means that when you receive your sample, it isn't just a "close match," it's a production-ready blueprint that guarantees a stable bulk run.
Your Partner in Global Fashion Growth
Scaling your brand shouldn't mean sacrificing oversight. We offer low MOQ flexibility that allows you to test new designs with minimal risk, then scale to full bulk production seamlessly. Our team provides dedicated support for fabric sourcing and trim management, ensuring every component meets your durability and color requirements. We act as the engine that powers your creative vision, providing a stable, transparent foundation for your global growth. Our partnership is built on the physical reality of the manufacturing facility, ensuring you feel supported from the initial concept to the final delivery.
Building a Resilient Remote Production Ecosystem
Transitioning to a remote oversight model is a strategic necessity for brands aiming to scale in 2026. You've seen how a "Sealed Golden Sample" serves as your technical anchor and why a structured inspection workflow from the pre-production meeting to the final random audit eliminates guesswork. By shifting from reactive audits to proactive factory partnerships, you protect your margins against rising fabric costs and high return rates. Managing remote quality control for apparel is no longer a hurdle; it's a competitive advantage when backed by the right technical infrastructure and digital transparency.
Success in the fashion industry requires a "safe pair of hands" that can translate creative vision into industrial reality. Ready to secure your supply chain? Partner with PowerSweet Fashion for Reliable Remote Production. We provide a 10-day sample turnaround and low MOQ flexibility to keep your brand agile in a fast-paced market. Our commitment to end-to-end transparency ensures you stay in control of every stitch and seam without ever needing to be on-site. Your brand deserves a production partner that values technical precision and open communication as much as you do.
Frequently Asked Questions
What is the most important document for remote quality control?
The production-ready Tech Pack is the most critical document because it serves as your technical contract for every specification. It must be paired with the Sealed Golden Sample, which acts as the physical benchmark for the factory. Together, these tools eliminate ambiguity by providing a clear pass/fail standard. Managing remote quality control for apparel is impossible without these benchmarks, as they ensure the factory has a precise target for bulk production.
How do I handle quality disputes with an offshore factory?
Use your AQL standards and the Sealed Golden Sample as objective evidence to resolve disputes. If a batch deviates from the agreed-upon sample, document the specific measurements or defects with high-resolution photos and video calls. Referencing the signed pre-production agreement helps keep the conversation professional and results-oriented. A transparent partner will work with you to find a solution, whether that involves rework or a credit, rather than ignoring the technical deviation.
Can I manage quality control effectively for low MOQ orders?
You can manage quality control more effectively for low MOQ orders because the smaller volume allows for a higher percentage of garments to be inspected. Low MOQs reduce your overall risk profile and make it easier to catch errors before they scale. This approach is ideal for growing brands that prioritize meticulous care over mass production. It allows you to refine your technical standards iteratively with your manufacturer during each production cycle.
What are AQL standards and how do I set them for my brand?
Acceptable Quality Level (AQL) standards are statistical sampling limits used to determine if a production run passes or fails. For most apparel brands, the industry standard is AQL 2.5 for major defects and 4.0 for minor cosmetic issues. You set these by defining what constitutes a "major" flaw, such as a hole or incorrect sizing, versus a "minor" flaw like a loose thread. These limits should be contractually agreed upon before production begins.
How often should I request production updates and photos?
You should establish a daily communication cadence for general updates via Slack or WhatsApp, but formal photo reviews are best requested at key milestones. Request detailed imagery during the "Top of Production" (TOP) phase and again at the 20-30% completion mark. This ensures you catch material or construction errors early without overwhelming the production team. Consistent, scheduled updates build a transparent partnership and provide empirical reliability throughout the manufacturing journey.
Is a third-party inspection always necessary for remote manufacturing?
A third-party inspection is not always necessary if you have a transparent, end-to-end production partner with robust internal standards. While independent audits provide unbiased verification for new factory relationships, they can be costly and lack design context. If your manufacturer offers "Open-Door Transparency" and live video walkthroughs, you can often achieve the same level of precision through direct oversight. The necessity depends on your trust level and the order's technical complexity.
What specific tools can help with remote garment measurements?
Digital calipers and standardized measurement tapes are essential for verifying garment dimensions in high-resolution photos. Using a color-calibrated monitor and Pantone swatches helps ensure color accuracy across different lighting environments. Additionally, Product Lifecycle Management (PLM) software or specialized apps like Techpacker allow you to log defects and measurements in a centralized digital hub. These tools bridge the physical distance by providing clear, data-driven evidence for managing remote quality control for apparel.


Comments